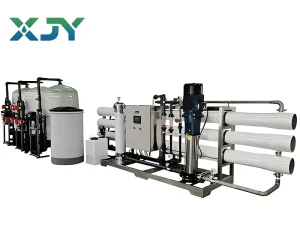
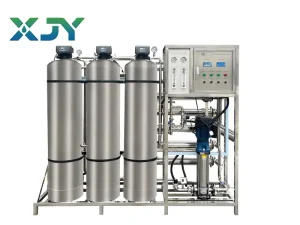
High-performance engineering hardware designed for robust industrial separation and purification.
The global mining industry faces unprecedented regulatory pressure regarding acid mine drainage (AMD), heavy metal contamination, and total dissolved solids (TDS) management. Enterprise procurement officers across North America, Latin America, Australia, and Asia-Pacific are shifting away from conventional, energy-intensive neutralization ponds toward automated, modular, and AI-optimized purification infrastructure. Modern mine water treatment is no longer merely a compliance obligation; it is a vital operational asset that dictates social license to operate (SLO) and ESG performance metrics.
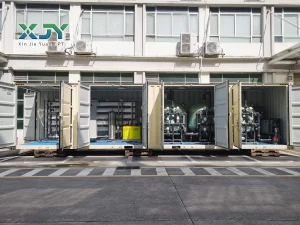
Key global enterprise procurement demands focus on modular containerized systems, rapid deployment capabilities, chemical reagent optimization, and Zero-Liquid Discharge (ZLD) configurations. Guangdong Xinjieyuan Environmental Protection Technology Co., Ltd. answers these demands through precision engineering, combining robust mechanical durability with smart PLC automation to lower Total Cost of Ownership (TCO).
Guangdong Xinjieyuan Environmental Protection Technology Co., Ltd. specializes in the R&D and manufacturing of elite environmental protection equipment. Operating at the forefront of water treatment, waste gas purification, and sewage sludge management, XJY represents a fully integrated enterprise uniting scientific research, production, and sales.
Our organization is built upon a proven professional operation team and extensive project execution capability across global industrial hubs. We hold professional contracting qualifications for environmental engineering, safety production licenses, and ISO quality, environmental, and occupational health management system certifications. With over 45 product patents and 32 computer software copyrights, our technological roadmap delivers unmatched reliability.
Integrated environmental engineering ecosystems engineered for maximum resource recovery.
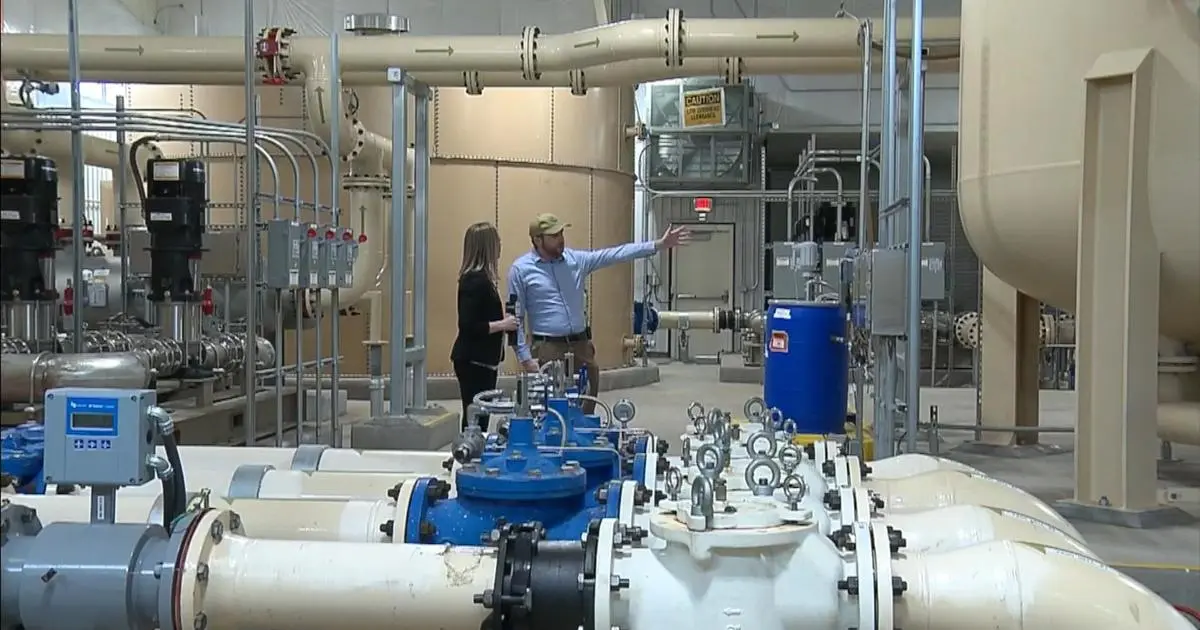
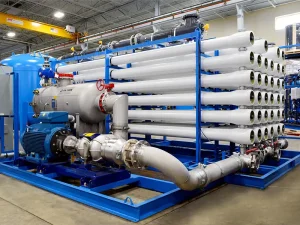
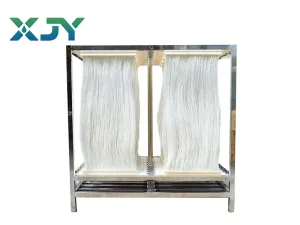
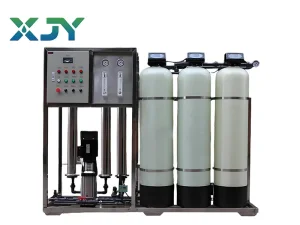
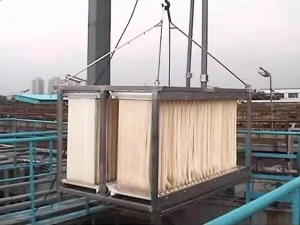
Developed with our proprietary "WPS Intelligent Water Purification System", providing precision treatment for mining wastewater, heavy metal effluents, and municipal supplies, driving energy conservation and water reuse.
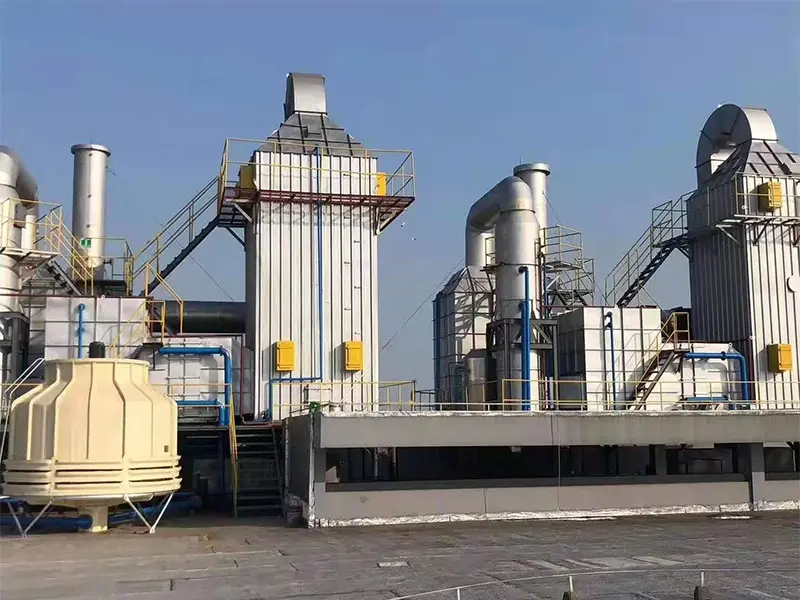
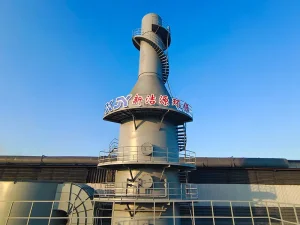
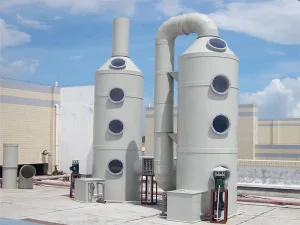
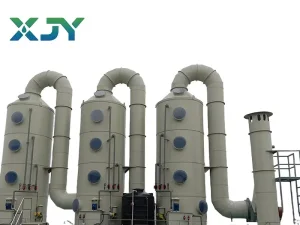
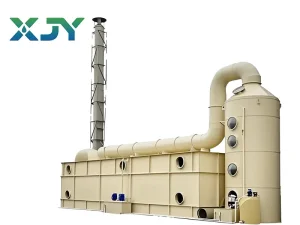
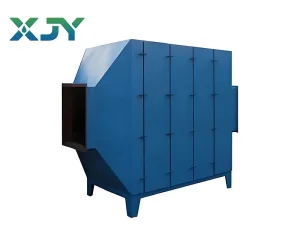
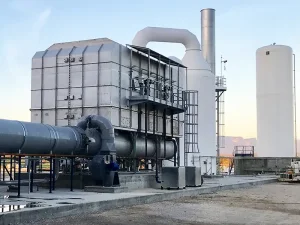
Featuring the "BDS Intelligent Deodorization System", specifically tailored to eradicate volatile organic compounds (VOCs) and chemical odors in mining operations, chemical plants, and municipal facilities.
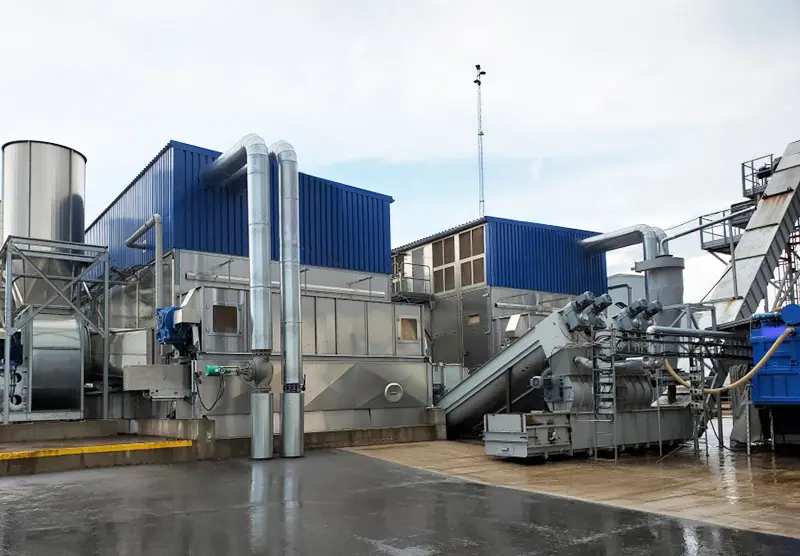
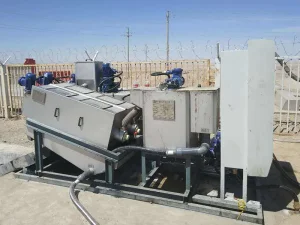
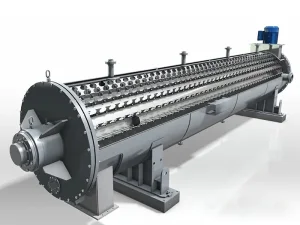
Turning high-moisture (80%) hazardous sludge into manageable dried granular raw materials (35% moisture) for resource reuse in cement and thermal power plants.
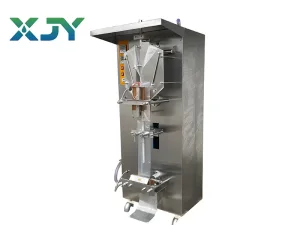
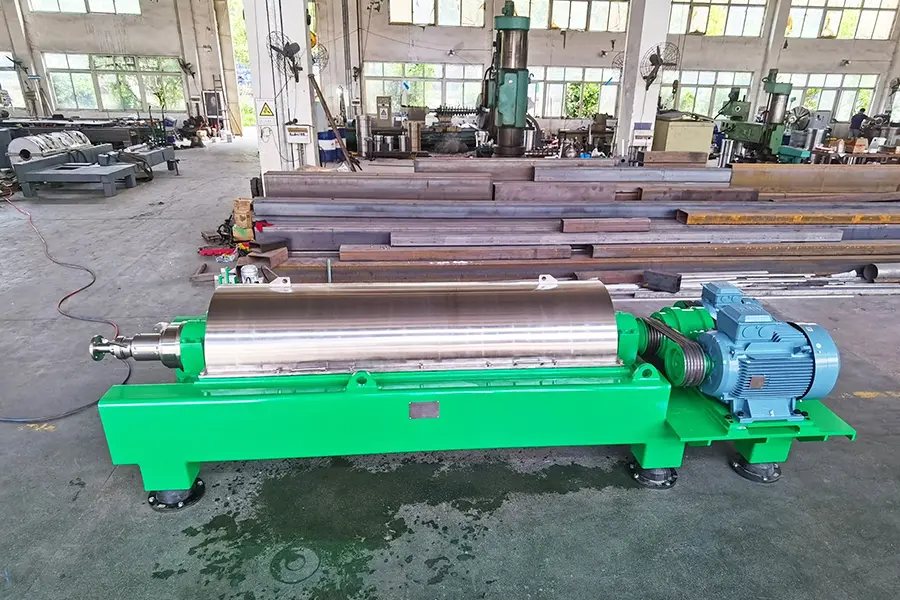
Specialized factory-direct machinery engineered for heavy-duty industrial processing.
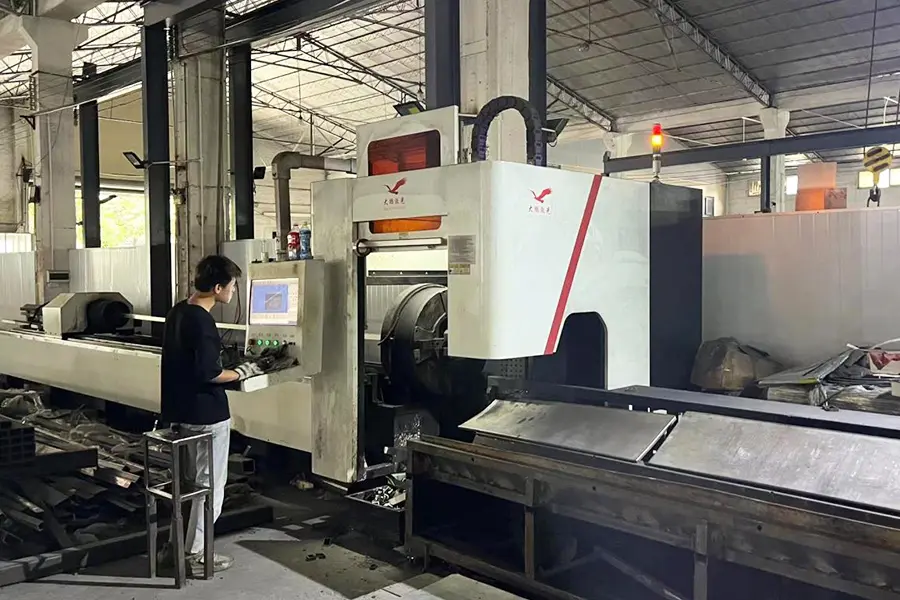
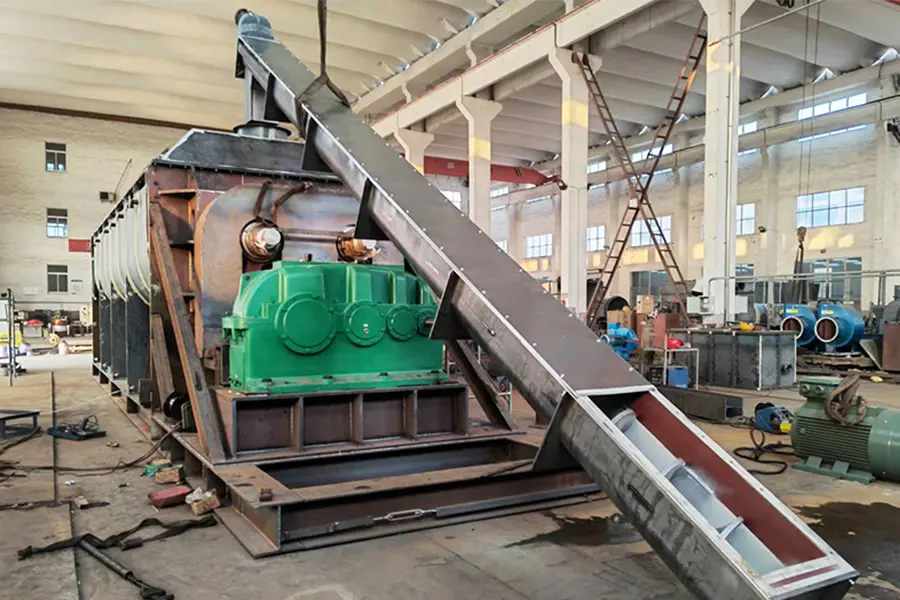
Our advanced manufacturing facility spans massive production floors equipped with automated CNC laser cutting machines, robotic welding arrays, and high-precision hydrostatic testing rigs. Every mine water treatment system undergoes rigorous factory acceptance testing (FAT) to simulate extreme heavy metal loading and high-salinity stress conditions before dispatch.
Committed to international standards, our products comply with strict global environmental regulations (EPA, EU Water Framework Directive, and ISO standards). We provide localized technical support, turnkey installation, operator training, and spare parts availability worldwide, ensuring long-term operational continuity for mining conglomerates.
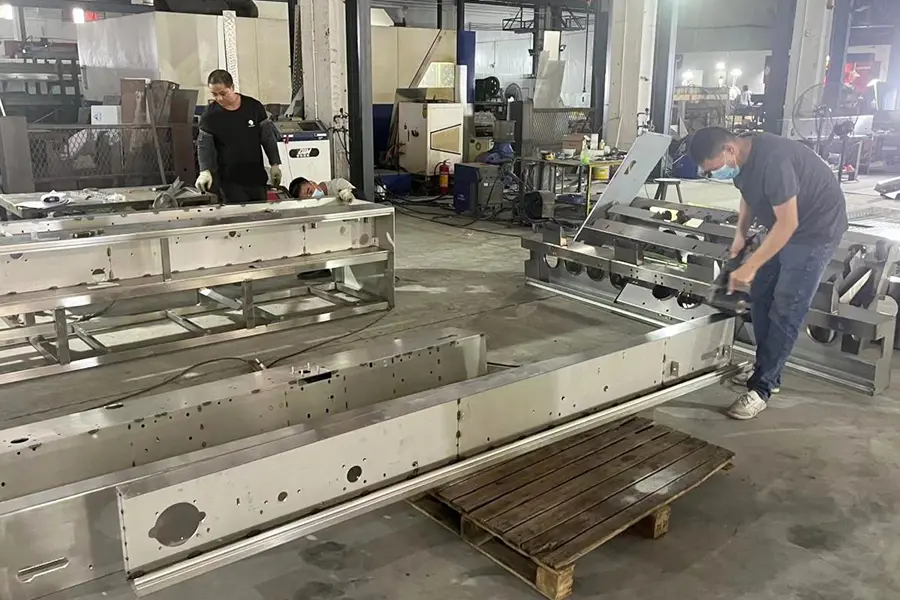
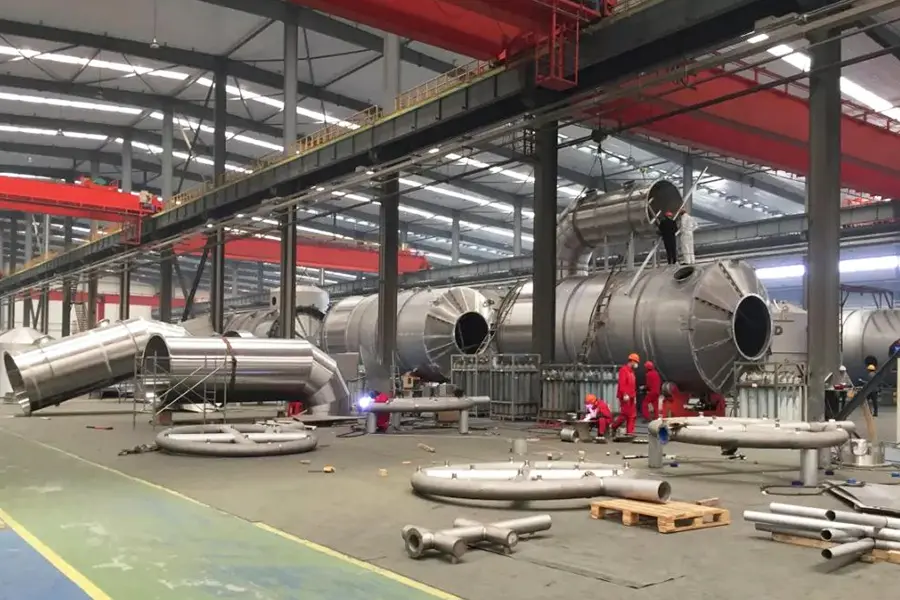
Visual verification of our manufacturing excellence and advanced fabrication capabilities.
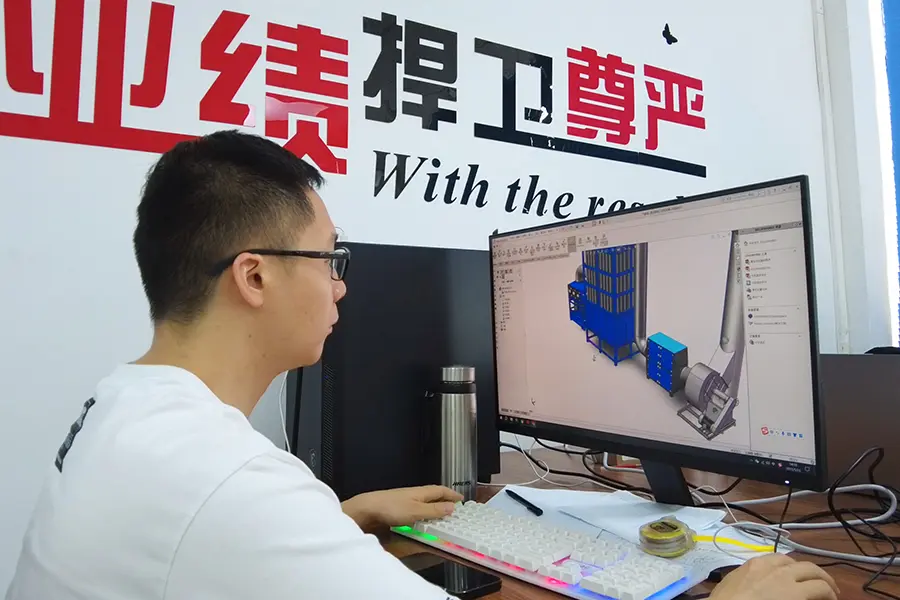
Expert insights on mine water treatment engineering, procurement, and maintenance.
 XINJIEYUAN